

Best China Extruded Heat Sink Manufacturer or Supplier?
Choosing the best China Extruded Heat Sink manufacturer or supplier requires more than comparing catalog prices. Thermal performance depends on alloy, profile geometry, surface treatment, machining accuracy, and assembly quality.
Industry data supports this demand. MarketsandMarkets reports that the global heat sink market is expanding as electric vehicles, data centers, LED systems, and power electronics require stronger thermal control. Grand View Research also identifies rising electronics density as a major market driver. These reports indicate opportunity, but they do not prove that every supplier can deliver consistent performance.
The details matter.
A reliable China Extruded Heat Sink partner should demonstrate aluminum alloy traceability, controlled extrusion tolerances, thermal testing, and repeatable anodizing quality. Requesting mill certificates, sample reports, and production photographs can reveal more than a polished website. In a real factory, the extrusion die may show wear, the cutting edge may leave burrs, and packaging may affect the finished surface. Small details become expensive problems.
Dr. Avram Bar-Cohen, a recognized thermal-management researcher, has repeatedly emphasized that “thermal management is a system-level issue.” His view is important because a heat sink cannot compensate for poor airflow, weak interface materials, or incorrect mounting pressure.
Supplier selection should therefore connect design capability with manufacturing evidence. Ask about thermal resistance testing, CNC capacity, minimum order quantities, and corrective-action procedures. ISO 9001 certification helps, but certification alone is not proof of engineering strength.
I may be too cautious. Yet caution is useful here. The lowest quotation can hide tooling costs, unstable tolerances, or inconsistent surface treatment. The best supplier is not always the largest one. It is the partner that can explain the numbers, reproduce the sample, and improve when the first design is imperfect.
What Is an Extruded Heat Sink and How Does It Work?
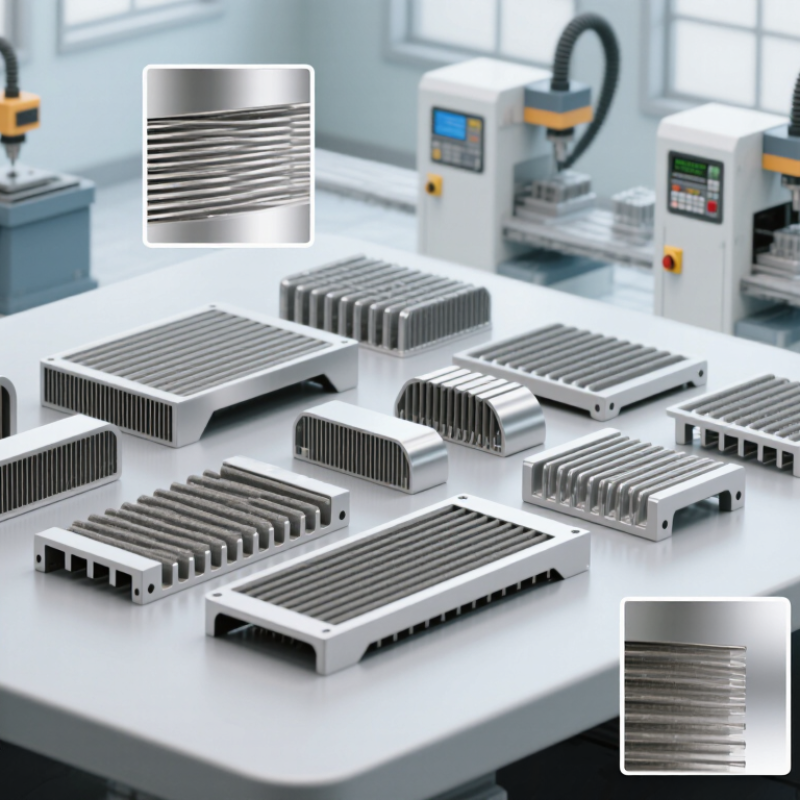
An extruded heat sink is a metal component that removes heat from electronic devices. It is commonly formed by pushing heated aluminum through a shaped die. This process creates a long profile with fins, grooves, or other cooling features. The profile is then cut to the required length. Aluminum works well because it is lightweight, conductive, and easy to process. The design may look simple. It is not.
When a processor or power module heats up, thermal energy moves into the heat sink through a thermal interface material. The sink spreads that energy across its base and fins. The fins provide more surface area for air contact. Natural airflow removes heat slowly, while a fan improves heat transfer. Fin spacing must match the airflow condition. Tight fins may perform well with strong forced airflow but struggle in passive cooling. Base flatness and mounting pressure also matter. A small contact gap can reduce real performance.
A capable manufacturer or supplier should discuss alloy selection, extrusion tolerances, surface treatment, and cutting accuracy. Ask for thermal test data under conditions similar to your application. One common mistake is choosing the tallest fins without checking airflow resistance. More metal does not always mean better cooling. I have seen compact designs outperform larger ones after improving contact quality and airflow direction. Still, calculations alone can mislead. Prototype testing remains essential, especially when heat loads change during operation.
Best China Extruded Heat Sink Manufacturer or Supplier? - What Is an Extruded Heat Sink and How Does It Work?
| Data Dimension | Typical Information | Why It Matters |
|---|---|---|
| Definition | An extruded heat sink is a thermal management component manufactured by forcing a heated metal billet through a shaped die to create a continuous finned profile. | The continuous profile provides a base and fins that transfer heat from an electronic component to the surrounding air. |
| Working Principle | Heat flows from the device into the mounting surface, spreads through the metal base, travels into the fins, and is released by natural convection or forced airflow. | A larger effective fin area and sufficient airflow generally improve heat dissipation. |
| Common Material | Aluminum alloys are widely used because they combine relatively high thermal conductivity, low density, corrosion resistance, and good extrudability. | Material selection affects thermal performance, weight, corrosion behavior, cost, and manufacturability. |
| Typical Aluminum Thermal Conductivity | Approximately 150–235 W/m·K, depending on alloy, temper, and material condition. | Higher conductivity can reduce temperature differences within the heat sink, although geometry and airflow are also critical. |
| Manufacturing Process | Billet preparation → heating → extrusion through a die → cooling → cutting → straightening or aging → surface treatment → inspection. | A controlled process helps maintain dimensional accuracy, fin consistency, surface quality, and repeatable thermal performance. |
| Fin Geometry | Typical designs include straight fins, parallel fins, slotted fins, pin-fin sections, and custom profiles. | Fin height, thickness, spacing, and orientation influence airflow resistance and available cooling area. |
| Cooling Method | Natural convection uses ambient airflow; forced convection uses a fan or blower to move air across the fins. | Forced airflow usually supports higher heat loads but adds noise, power consumption, and moving parts. |
| Typical Applications | LED lighting, power supplies, motor drives, inverters, industrial controls, telecommunications equipment, renewable-energy systems, and computing hardware. | Extruded profiles can be adapted to different mounting patterns, heat loads, enclosure sizes, and airflow conditions. |
| Main Advantages | Continuous production, customizable cross-sections, relatively low tooling cost, good strength-to-weight ratio, and easy cutting or machining. | These benefits make extrusion suitable for both standard profiles and medium-to-large production volumes. |
| Design Limitations | Very high or very thin fins may be difficult to extrude; deep cavities, abrupt wall changes, and complex three-dimensional shapes may require another process. | Designing within extrusion constraints can improve yield, reduce tooling stress, and control production costs. |
| Surface Treatments | Common options include anodizing, chemical conversion coating, powder coating, painting, and untreated mill finish. | Finishes can improve corrosion resistance, appearance, electrical insulation, or emissivity, but coating thickness may affect thermal contact and tolerances. |
| Key Selection Criteria | Heat load, allowable component temperature, ambient temperature, available space, airflow, mounting method, material, surface treatment, tolerances, and required quantity. | A heat sink should be selected from the complete thermal system rather than by size or material alone. |
| Supplier Evaluation Points | Extrusion capability, die-design support, alloy control, dimensional inspection, thermal testing, machining capacity, surface-treatment control, packaging, and export documentation. | These factors help verify whether a supplier can consistently meet engineering, quality, and delivery requirements. |
| Performance Verification | Review dimensional inspection records, material certificates, surface-finish results, thermal-resistance data, airflow test conditions, and sample approval results. | Thermal results are meaningful only when test power, orientation, airflow, interface material, and ambient conditions are clearly stated. |
| Note: Material properties and thermal performance are typical industry ranges or general engineering guidance. Actual results depend on alloy, profile geometry, surface treatment, contact resistance, installation orientation, heat load, and airflow conditions. | ||