Language:

What Is Nev Aluminum Machining and How Does It Work?

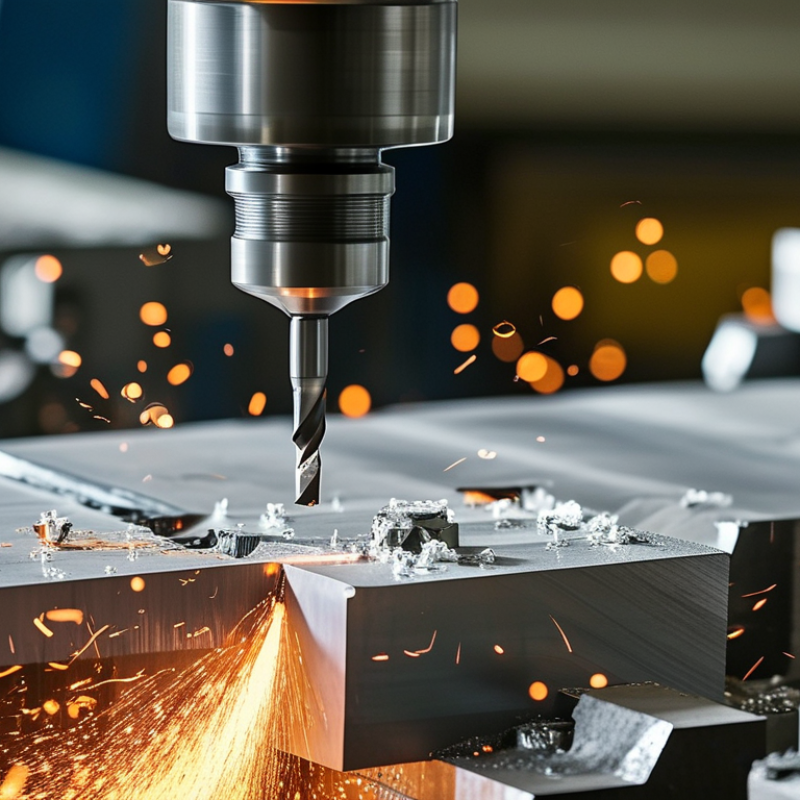
Nev Aluminum Machining describes the controlled cutting, drilling, milling, and finishing of aluminum components. The process turns digital designs into accurate physical parts. It often uses CNC equipment, carbide tools, coolant, inspection instruments, and carefully selected cutting parameters. Aluminum appears soft compared with steel, but it can still challenge machinists. It may smear, form built-up edges, or vibrate inside thin sections.

Manufacturing expert Dr. Thomas Kurfess describes the broader purpose of advanced production: “Manufacturing is the process of turning ideas into products.” That principle fits Nev Aluminum Machining closely. A machinist begins with an aluminum grade, such as 6061-T6 or 7075-T6, then studies the drawing, tolerances, surface requirements, and production volume. The machine removes material along programmed toolpaths. Probes, calipers, micrometers, and coordinate measuring machines verify the result.

Small details matter.

A sharp tool can leave a bright, even surface. A worn tool may create streaks, burrs, or unwanted heat. Thin walls can flex during cutting, causing dimensions to drift after clamping pressure is released. This is where practical experience becomes valuable. Software predicts motion, but it cannot always predict every vibration, chip, or material inconsistency.

That description remains incomplete. Nev Aluminum Machining is not simply automated cutting. It combines engineering judgment, process control, operator experience, and documented inspection. Reliable work requires traceable materials, calibrated equipment, realistic tolerances, and honest quality reporting. The following sections explain how the process works, where defects appear, and how professional shops improve accuracy without sacrificing efficiency.
What Is Nev Aluminum Machining and How Does It Work?

Definition and Basic Principles of NEV Aluminum Machining

What Is Nev Aluminum Machining and How Does It Work?

NEV aluminum machining means shaping aluminum parts for new energy vehicles through controlled cutting processes. NEV usually refers to electric, hybrid, and other new energy vehicles. The work begins with an engineering drawing, material grade, and required dimensions. A CNC machine then removes material from a billet or casting. Milling creates pockets and flat surfaces, while turning produces round components.

The basic principle is simple: a cutting tool removes small chips along programmed paths. Machine speed, feed rate, and cutting depth must match the aluminum alloy. Excessive speed can create heat and rough edges. Too little feed may rub the surface instead of cutting it. Coolant or air helps control temperature and clear chips from narrow grooves. Burrs can still appear. They require careful deburring.

Accuracy depends on more than computer control. Tool wear, fixture movement, and material expansion can change the final size. Technicians check critical features with calipers, micrometers, or coordinate measuring equipment. They may inspect a hole near a battery housing or a thin wall inside a motor cover. A perfect first pass is not guaranteed. In practice, experienced machinists adjust the program after reviewing measurements. This human review remains important, especially when tight tolerances and clean sealing surfaces are required.
Key Aluminum Alloys, Machines, and Cutting Tools

Nev aluminum machining depends heavily on alloy selection. Aluminum 6061 is a practical choice for brackets, housings, and general components. It cuts cleanly and offers a useful balance of strength and corrosion resistance. Aluminum 7075 is stronger, but it can demand sharper process control. Its reduced corrosion resistance also matters in outdoor designs. Aluminum 2024 machines well, though its copper content requires careful surface protection. Softer 5052 works better for formed parts than tight-tolerance milling.

Machine choice shapes the final result. A three-axis CNC mill handles many flat profiles and pockets. A five-axis machine reaches angled surfaces with fewer setups. CNC lathes suit round shafts, sleeves, and threaded features. High spindle speed helps aluminum, but excessive speed can create built-up edge. Carbide end mills with polished flutes usually evacuate chips effectively. Two- or three-flute cutters leave more space for chip flow. Coolant, air blast, or minimum-quantity lubrication can prevent chips from welding to the tool.

Tool geometry deserves close attention. A variable helix can reduce vibration on thin walls. Drills should clear chips often, especially in deep holes. Reamers improve size consistency after drilling. Sharp tools matter more than impressive machine power. No setup is perfect. In practice, thin sections may spring back after cutting, and a final inspection can reveal unexpected distortion. Measuring critical features during machining is safer than trusting the first successful part. Cutter wear, workholding pressure, and temperature should remain part of the process record.

Step-by-Step Workflow of the Machining Process

Nev Aluminum Machining: Step-by-Step Workflow of the Machining Process

Nev aluminum machining is a controlled method for shaping aluminum parts with cutting tools and computer-guided equipment. The workflow begins with a technical drawing, three-dimensional model, or approved sample. Engineers check dimensions, tolerances, hole positions, and surface requirements before programming the machine. Aluminum is relatively soft, but it can still deform, smear, or build material on the cutter.

Material preparation comes next. The operator selects an aluminum grade, cuts the blank, and secures it firmly on the worktable. Poor clamping can cause vibration and inaccurate edges. The machine then removes material through milling, drilling, facing, or turning operations. Cutting speed, feed rate, and tool condition must match the alloy and part geometry. Coolant or controlled air can reduce heat and help clear chips.

The process needs careful observation.

After rough cutting, technicians measure critical features with calipers, micrometers, or coordinate equipment. They compare actual results with the drawing and adjust tool offsets when necessary. Finishing passes create sharper edges and a more consistent surface. Deburring removes thin, dangerous fragments around holes and corners. An imperfect setup may still produce a usable part, but it should not be accepted without investigation. Even a small measurement error can affect assembly, sealing, or long-term performance. Final inspection records dimensions, appearance, and any corrective action before the component moves to cleaning and packaging.

What Is CNC Aluminum Machining and How Does It Work?

A typical machining workflow converts a digital design into a finished aluminum component through planning, setup, material removal, finishing, and inspection.

The chart shows representative production-time allocation for a small-to-medium CNC-milled aluminum part. Actual timing varies with part geometry, tolerances, alloy, tooling, machine capacity, and batch size.

Critical Parameters Affecting Machining Quality

What Is NEV Aluminum Machining and How Does It Work?

Critical Parameters Affecting Machining Quality

NEV aluminum machining produces lightweight housings, motor parts, and structural components for new-energy vehicles. Quality depends heavily on cutting speed, feed rate, depth of cut, and tool geometry. Aluminum removes quickly, but it can smear when heat rises or chips recut. The International Aluminium Institute reports that recycled aluminum requires about 5% of the energy used for primary aluminum production. However, recycled material may show wider chemistry variation, so machinists should verify hardness and composition before setting parameters.

Cutting speed must match alloy, cutter diameter, and coating. Excessive speed can create built-up edges. Low feed rates may polish the surface instead of cutting cleanly. A stable starting point often uses sharp carbide tools, a positive rake angle, and continuous chip evacuation. Coolant helps, but poor delivery can still leave hot spots. Small details matter.

Fixturing also affects accuracy. Thin walls can distort after release, even when the part measured correctly on the machine. Temperature matters too. ISO 1 measurement conditions commonly use 20°C, while production floors rarely remain perfect. That gap deserves attention. The Aluminum Association’s statistical reviews show aluminum demand remains substantial across transportation manufacturing, increasing pressure for repeatable, low-waste machining. In practice, operators should record spindle load, tool wear, surface roughness, and dimensional drift after each batch. One parameter rarely explains every defect.

Applications, Benefits, and Common Limitations

What Is NEV Aluminum Machining and How Does It Work?

NEV aluminum machining produces precise components for new energy vehicles. The process begins with a digital design and selected aluminum alloy. Technicians secure the material before milling, turning, drilling, or cutting it. Cutting speed, tool geometry, and coolant flow require careful adjustment. Small changes can affect dimensional accuracy.

Battery trays, motor housings, cooling plates, suspension brackets, and structural panels commonly use machined aluminum. The material offers low weight, good thermal conductivity, and practical corrosion resistance. These qualities can improve vehicle efficiency and help manage battery heat. Machining also supports quick prototypes and small production batches. Engineers can inspect each critical surface with coordinate measuring equipment.

The method has limitations. Aluminum removes quickly, but it can create long chips and unwanted burrs. Thin walls may vibrate during cutting. Heat can also cause expansion and misleading measurements. A part may pass a visual check yet fail a tight assembly test. That happens more often than expected. Porosity inside cast material can weaken drilled areas, while complex shapes increase fixture and programming costs. Surface finish may require extra deburring or treatment. Tool wear is another concern, especially during high-volume production. Experienced machinists usually review wall thickness, clamping points, tolerances, and heat paths before cutting. Even then, the first design is rarely perfect. A practical trial often reveals problems that drawings do not show.

What Is CNC Aluminum Machining and How Does It Work? - Applications, Benefits, and Common Limitations

Category Key Information Typical Considerations
Definition CNC aluminum machining is the computer-controlled cutting, drilling, boring, tapping, or milling of aluminum stock to create precise components. It can produce prototypes and repeatable production parts with complex profiles and close dimensional control.
How the Process Works A 3D CAD model is converted into CAM toolpaths and machine code. The CNC machine then removes material using rotating cutting tools while the workpiece is securely held. Tool selection, workholding, cutting parameters, coolant, and inspection all affect the final result.
Common Machine Types Three-axis and five-axis machining centers, CNC lathes, turning centers, routers, and mill-turn machines are commonly used. Three-axis equipment suits many prismatic parts; five-axis equipment can reduce setups for angled and highly contoured features.
Frequently Machined Aluminum Alloys 6061 is widely used for general-purpose parts, 7075 is selected for higher strength, 2024 is used where strength-to-weight performance is important, and 5052 is commonly used for formed or corrosion-resistant components. The best alloy depends on strength, corrosion resistance, machinability, weldability, surface finish, and cost requirements.
Material Characteristics Aluminum is lightweight, electrically and thermally conductive, and generally easier to cut than many steels. Its relatively low stiffness can increase vibration or deflection when thin walls, long tools, or poorly supported workpieces are used.
Typical Dimensional Capability General CNC milling tolerances are often specified around ±0.пай01 in to ±0.005 in (approximately ±0.025 to ±0.127 mm), depending on the machine, geometry, material, and inspection method. Tighter tolerances require suitable design, stable fixturing, controlled temperature, additional finishing passes, and verification. Actual capability must be confirmed for each part.
Surface Finish Machined aluminum can provide a clean functional finish; the result depends on tooling, feed rate, spindle speed, toolpath, alloy, and part rigidity. Anodizing, bead blasting, brushing, polishing, or chemical conversion coating may be used for appearance, wear resistance, or corrosion protection.
Main Applications Enclosures, brackets, heat sinks, manifolds, robotics components, automation fixtures, camera and optical mounts, lightweight structural parts, and transportation components. Aluminum is particularly useful where low mass, precise geometry, thermal performance, or corrosion resistance is needed.
Primary Benefits High strength-to-weight ratio, good machinability, rapid material removal, repeatable production, design flexibility, and compatibility with many finishing processes. It is often suitable for prototypes and low- to medium-volume production without the tooling investment required by many molding processes.
Common Limitations Material waste can be significant for parts machined from solid stock, and very thin features may deform. Aluminum also has a lower elastic modulus than steel. Deep cavities, sharp internal corners, long unsupported walls, and difficult-to-reach features may increase machining time, tooling requirements, or cost.
Design-for-Machining Guidelines Use internal radii compatible with cutting tools, avoid unnecessarily deep pockets, maintain adequate wall thickness, and provide clear tool access. Reducing setups and avoiding exceptionally tight tolerances can improve lead time, manufacturability, and cost.
Quality Control Inspection may include calipers, micrometers, height gauges, optical systems, coordinate-measuring machines, and surface-finish instruments. Inspection requirements should identify critical dimensions, datums, geometric tolerances, material condition, and surface-finish specifications.
Best Fit for CNC Aluminum Machining It is a strong option for accurate, lightweight, customized parts with moderate or complex geometry and changing production requirements. Alternative processes may be more economical for very high volumes, extremely simple shapes, or parts requiring extensive forming rather than material removal.

Note: Tolerance ranges and manufacturing results are application-dependent. Final specifications should be confirmed through engineering drawings, material certifications, machine capability studies, and inspection requirements.

Member of

Associated Wire Rope FabricatorsMHI MemberNetPlus Alliance Member Steel Erectors Assocation STADFA member

Terms of Sale | Privacy Policy