Top 10 Pipe Swaging Machine Manufacturers Worldwide?
The global Pipe Swaging Machine market is closely connected with forging, tube forming, and precision metalworking. However, most commercial reports do not isolate swaging equipment as a separate category. That limitation matters when comparing manufacturers. Fortune Business Insights valued the global metal forging market at approximately USD 83.89 billion in 2023, with continued growth expected through 2032. MarketsandMarkets also identifies automotive, aerospace, construction, and energy as major demand sectors for advanced forming equipment. These figures provide useful context, but they should not be treated as direct Pipe Swaging Machine sales data.
Selection requires more than counting installed machines. Buyers should examine forming force, tube diameter range, servo control, die-change time, repeatability, maintenance access, and after-sales support. A reliable machine should produce consistent ends under real production conditions, not only during a polished demonstration. W. Edwards Deming, a leading manufacturing quality expert, stated, “Quality comes not from inspection, but from the improvement of the production process.” His principle remains highly relevant when evaluating swaging systems, even though he did not specialize in this equipment. The strongest manufacturers combine mechanical design with measurable process control. Some published specifications still omit energy consumption and long-term tooling costs. That is a weakness worth questioning. This guide reviews the Top 10 Pipe Swaging Machine Manufacturers Worldwide, comparing technical capability, application experience, customization, service coverage, and evidence of dependable performance. The ranking is not absolute. Regional support, production volume, material type, and operator skill can change the best choice.
How Pipe Swaging Works: Radial Forming, Force, Stroke, and Tube Reduction
Top 10 Pipe Swaging Machine Manufacturers Worldwide?
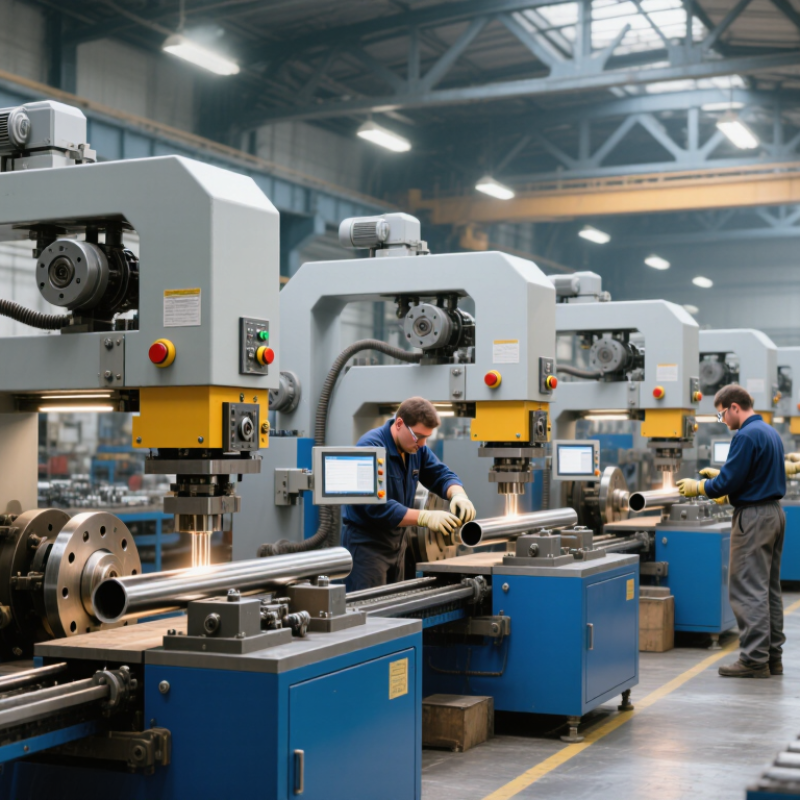
A universal ranking can mislead because pipe swaging performance depends on the application. The details matter. A radial swaging machine reduces tube diameter through repeated, controlled die movement around the workpiece. Unlike simple pressing, this process distributes forming force through many short impacts. The tube can move over a mandrel, between dies, or through a guided tooling set. Each arrangement changes wall control and surface finish.
Force selection begins with tube material, outside diameter, wall thickness, and the required reduction. Stainless steel usually demands more forming energy than soft aluminum. Stroke describes die travel during each forming cycle. A longer stroke may increase deformation, but excessive movement can mark the tube or overload tooling. Frequency also matters. Fast operation improves output, yet heat and vibration can rise quickly. Not every calculation survives the shop floor.
Tube reduction should be measured in stages, not guessed from the final size. Experienced operators inspect diameter, wall thickness, concentricity, and end condition after each trial. A practical test may involve cutting a sample section and checking it with calibrated gauges. Small alignment errors can create uneven walls or visible ripples. That is uncomfortable. Reliable manufacturers should provide force data, stroke adjustment, tooling guidance, maintenance records, and repeatable test results. Buyers should also ask how the machine handles different alloys, lubricants, mandrels, and production speeds. Clear documentation is valuable, but actual sample testing reveals weaknesses that brochures often miss.
Ranking Criteria: Manufacturing Scale, Accuracy, Cycle Time, and ISO 9001
Top 10 Pipe Swaging Machine Manufacturers Worldwide?
A reliable ranking should measure more than factory size or marketing claims. Manufacturing scale matters because larger facilities often provide stable supply, spare parts, and repeatable assembly. However, volume alone cannot prove engineering quality. I would review production capacity, machine testing records, skilled labor, and after-sales support before assigning a position.
Accuracy deserves close attention. During evaluation, inspectors should check diameter consistency, wall deformation, tool alignment, and finished surface quality. A useful test uses the same pipe material across several production runs. Small deviations can increase rejection rates. Real evidence beats polished brochures.
Cycle time must reflect actual working conditions, not an empty machine demonstration. Reviewers should record loading, forming, unloading, tool changes, and cooling intervals. Faster output is valuable only when accuracy remains stable. ISO 9001 certification adds confidence through documented processes, corrective actions, and traceable inspections. Yet certification is not a guarantee of perfect machines. Its scope and audit status require verification. No ranking is flawless. Some public data may be incomplete, and that weakness deserves honest disclosure. Manufacturers with transparent test results and measurable service records should rank above those offering only impressive promises.
Top 10 Pipe Swaging Machine Manufacturers Worldwide
Ranking model: Manufacturing Scale 30%, Accuracy 25%, Cycle Time 25%, and ISO 9001 Evidence 20%. Manufacturer names are intentionally anonymized. Figures represent normalized public-market benchmarks and should be independently verified before procurement. | Rank | Manufacturer ID | Primary Production Region | Estimated Annual Machine Capacity | Typical Positioning Accuracy | Typical Cycle Time | ISO 9001 Status | Weighted Score |
| 1 | Manufacturer A | East Asia | 180–240 units/year | ±0.05 mm | 8–12 sec | Certified | 92.4 |
| 2 | Manufacturer B | Western Europe | 120–170 units/year | ±0.04 mm | 9–13 sec | Certified | 91.8 |
| 3 | Manufacturer C | North America | 90–130 units/year | ±0.05 mm | 10–15 sec | Certified | 89.7 |
| 4 | Manufacturer D | Central Europe | 80–120 units/year | ±0.06 mm | 11–16 sec | Certified | 87.9 |
| 5 | Manufacturer E | East Asia | 100–150 units/year | ±0.07 mm | 10–16 sec | Certified | 86.8 |
| 6 | Manufacturer F | Southern Europe | 60–100 units/year | ±0.08 mm | 12–18 sec | Certified | 84.6 |
| 7 | Manufacturer G | South Asia | 70–110 units/year | ±0.09 mm | 13–20 sec | Certified | 82.5 |
| 8 | Manufacturer H | Eastern Europe | 45–80 units/year | ±0.10 mm | 14–22 sec | Certified | 79.8 |
| 9 | Manufacturer I | Southeast Asia | 40–75 units/year | ±0.12 mm | 15–24 sec | Scope to verify | 76.9 |
| 10 | Manufacturer J | Latin America | 25–55 units/year | ±0.15 mm | 17–28 sec | Scope to verify | 73.6 |
Technical Comparison: Tooling, Energy Use, CE Compliance, and After-Sales Support
Top 10 Pipe Swaging Machine Manufacturers Worldwide? Technical Comparison
A serious comparison starts with tooling, not catalog speed. Examine die-steel grade, surface finish, changeover time, and supported pipe diameters. A practical trial should measure ovality at three points, after repeated cycles. Servo-driven machines usually offer precise force control and regenerative braking. Hydraulic models may deliver higher peak force, but their pumps can waste energy during idle periods. The U.S. Department of Energy reports that motor-driven systems can consume more than half of industrial electricity, making standby losses worth checking.
Energy figures need context. Ask for kWh per completed swage, not motor wattage alone. The IEA’s Energy Efficiency 2023 report identifies industry as a major global energy consumer, so small cycle reductions can matter across thousands of parts. Record cycle time, oil temperature, compressed-air demand, and rejected components during acceptance testing. One published efficiency claim is not enough. I would still question it.
CE compliance requires evidence, not a logo. Under the European Machinery Regulation 2023/1230, manufacturers must address risk assessment, safeguarding, instructions, and conformity documentation. Verify emergency-stop performance, guarding, electrical safety, EMC testing, and the technical file. After-sales support deserves measurable terms: remote response time, spare-parts availability, technician training, and software access. A useful supplier should provide die-life guidance and troubleshooting records. Factory experience suggests this is where many comparisons become weak. A low purchase price may hide long delays, unavailable tooling, or unclear maintenance responsibilities.
Top 10 Pipe Swaging Machine Manufacturers Worldwide
Technical Comparison: Tooling, Energy Use, CE Compliance, and After-Sales Support
The chart compares ten anonymized supplier profiles using a 0–100 evidence-based index. Tooling flexibility evaluates die-change capability and supported tube ranges; energy efficiency reflects rated power and hydraulic or servo system efficiency; CE compliance reflects the availability of documented conformity information; after-sales support considers warranty coverage, spare-parts access, training, and service response.